Ceramic CNC Machining vs. 3D Printing: Which Process Should You Choose?

An Engineer’s Guide to Geometry, Tolerances, Production Economics and Hybrid Manufacturing: Which Process Should You Choose?

Technical ceramics are selected for demanding environments, but manufacturing them can be challenging. Should an engineer machine a part from fired ceramic stock, shape it before sintering, or use ceramic additive manufacturing? Drawing on 3DCeram Sinto’s experience in ceramic stereolithography and industrial process development, this guide compares CNC machining with ceramic 3D printing. The best choice depends on geometry, material requirements, precision, production volume and the complete manufacturing route—not simply on machine speed.

CNC Machining vs. Ceramic 3D Printing: Key Differences

CNC machining removes material using programmed cutting tools. For technical ceramics, the route may involve machining a pre-sintered (green or partially fired) blank, hard machining a sintered component, or a combination of both. Tool access, fixture design, abrasive wear and the risk of chipping or cracking can influence feasibility and cost.

Ceramic additive manufacturing instead shapes a part layer by layer from a digital design. In ceramic stereolithography (SLA) or digital light processing (DLP), light cures a ceramic-loaded slurry. 3DCeram Sinto specializes in ceramic SLA and develops both printing equipment and ceramic feedstocks. The printed green part then requires cleaning, debinding and sintering: printing alone does not produce a finished technical-ceramic component.

Neither process is universally easier. CNC concentrates much of its complexity in tooling, access and cutting strategy, while ceramic 3D printing moves significant complexity to part orientation, support design, slurry behavior and thermal post-processing.

Decision factor CNC machining of ceramics Ceramic SLA / DLP printing
Geometry Strong for accessible features; enclosed channels and deep recesses can be difficult. Enables intricate internal channels, lattice structures and complex integrated shapes, subject to cleaning and firing constraints.
Precision & finish Can achieve demanding finishes on accessible surfaces with appropriate equipment and process control. Final dimensions depend on shrinkage and firing; critical surfaces may require finishing.
Tooling & setup May require several fixtures, cutting tools and setups. Avoids geometry-specific molds; requires build preparation and post-processing equipment.
Production economics Often attractive for simpler designs, established routings or particular batch sizes. Can favor complex, customized or low-volume components; economics depend on throughput and yield.

Why Are Technical Ceramics Difficult to Machine?

Alumina, zirconia and other advanced ceramics combine valuable functional properties with demanding processing behavior. High hardness after sintering makes material removal difficult, while brittleness raises the possibility of edge chipping, microcracks or part rejection. Complex shapes may need multiple setups, specialist tooling or substantial material removal.

Machining before full sintering can ease cutting, but the part still changes dimension during firing. Hard machining after sintering can deliver precise interfaces, although it adds time and equipment demands. Manufacturers therefore need to assess the full sequence—not just the CNC cycle time.

When Does Ceramic 3D Printing Offer an Advantage?

The strongest argument for additive manufacturing is geometric freedom. Internal flow passages, lightweight lattices and consolidated multi-feature components may be difficult, costly or impractical to produce by subtractive methods. Digital production also reduces dependence on dedicated forming molds. 3DCeram’s SLA range supports this approach from development to industrial production: the C101 EASY FAB (100x100x150 mm) for smaller builds and process development, the C1000 FLEXMATIC (320x320x200 mm) for larger-scale production, and the C3601 ULTIMATE (600x600x300 mm) for large ceramic components and mass production.

However, additive manufacturing has its own design rules. Trapped slurry must be removable, fragile green features need adequate support, and debinding and sintering must suit the geometry. 3DCeram’s process expertise covers these critical steps as well as printing. A representative fired test part is essential before committing to production.

Big part in alumina printed on the 3DCERAM C3601 ULTIMATE showing complex geometries that 3D printing can make

Tolerances, Surface Finish, Costs and Production Volumes

Comparisons should be based on the finished, inspected ceramic part. CNC performance depends on tool access, machining stage, material and equipment. Ceramic SLA performance depends on exposure, orientation, cleaning, dimensional compensation and the firing cycle. For either route, specify the tolerances and roughness only where function requires them.

Cost per accepted part is more informative than machine time or quoted printing time. Include material use, tooling, operator time, cleaning, debinding, sintering, inspection, finishing and rejects. For straightforward, accessible geometries, CNC may remain the practical choice. As geometric complexity increases or tooling becomes burdensome, additive manufacturing can become more compelling.

Part requirement Route worth evaluating What to validate
Simple plate, slot or accessible bore CNC machining Stock availability, fixture stability, achievable tolerance and total unit cost.
Intricate channels or lattice Ceramic SLA / DLP Slurry evacuation, feature integrity, firing deformation and internal inspection.
Complex body with tight mating faces Additive + selective CNC finishing Machining allowance, datum strategy and final dimensions after firing.
Repeated series production Compare both using a pilot batch Throughput, process stability, yield and cost per conforming part.

Can CNC and Ceramic 3D Printing Work Together?

Yes. A hybrid production strategy can print near-net-shape ceramic geometry and then machine selected datums, sealing faces or bores. This combines additive design freedom with controlled finishing where it matters. The additional operations are justified only when they improve the performance or economics of the complete route.

3DCeram’s M.A.T. (Multi Additive Technology) platform illustrates the value of combining additive operations and CNC machining in one manufacturing approach. The specific process sequence and material compatibility must still be evaluated for each application; it should not be assumed that every fired ceramic feature can be machined in the same way.

Industrial Applications and Practical Process Selection

3DCeram applies ceramic additive manufacturing to demanding fields such as aerospace, semiconductor equipment, defense and energy. Semiconductor parts may require chemical stability, precise interfaces and complex functional geometries; aerospace and energy designs may benefit from lightweight structures or optimized flow paths. In every case, material properties, inspection requirements and production repeatability must be demonstrated on the final fired part.

Ceramic part for Aerospace application printed on the 3DCERAM C1000 FLEXMATIC.

Before choosing, answer five questions: Can a cutting tool reach every essential feature? Which material and fired properties are required? What tolerances and surface finishes are functionally critical? How many conforming parts are needed? And what cleaning, firing, finishing and qualification steps does each route involve?

Conclusion: Choose the Process, Not Just the Machine

CNC machining remains valuable for accessible, precision-critical ceramic features. Ceramic additive manufacturing expands what can be designed and can reduce the need for dedicated forming tools. Hybrid manufacturing may offer the best compromise when complex shapes need accurately finished interfaces. Compare both routes on validated final-part performance, repeatability and cost, not on headline process speed alone.

Evaluating a technical-ceramic component? Explore 3DCeram’s ceramic SLA solutions from the C101 EASY FAB to the C1000 FLEXMATIC and C3601 ULTIMATE alongside its M.A.T. hybrid platform, or contact the 3DCeram Sinto team to discuss material selection, part feasibility and the right manufacturing workflow.

Ceramic SLA 3D Printing: The Essential Guide

How to evaluate ceramic slurry, printer capability and production fit for industrial parts

Stereolithography (SLA) uses a laser to cure a light-sensitive material layer by layer. In ceramic 3D printing, that material is a slurry of ceramic powder and photosensitive binder. An SLA ceramic 3D printer forms a fragile “green” part; cleaning, binder removal and sintering turn it into the finished ceramic component. Choosing an SLA ceramic 3D printer means matching the machine, slurry and firing process to the part’s shape and intended use. This guide explains what to check when comparing systems and compatible materials.

From Slurry to Sintered Ceramic

What SLA Ceramic Resin Means

“SLA ceramic resin” is a common search phrase, but industrial ceramic feedstock is usually called a slurry or suspension. It combines ceramic powder with a photosensitive binder that lets a UV laser cure the slurry layer by layer. These formulations are not interchangeable with standard polymer resins, and a printer’s compatibility must be confirmed for the specific slurry, exposure settings and cleaning process. 3DCeram’s 3DMIX ceramic slurries are formulated for CERAMAKER systems, so the material and machine should be reviewed together

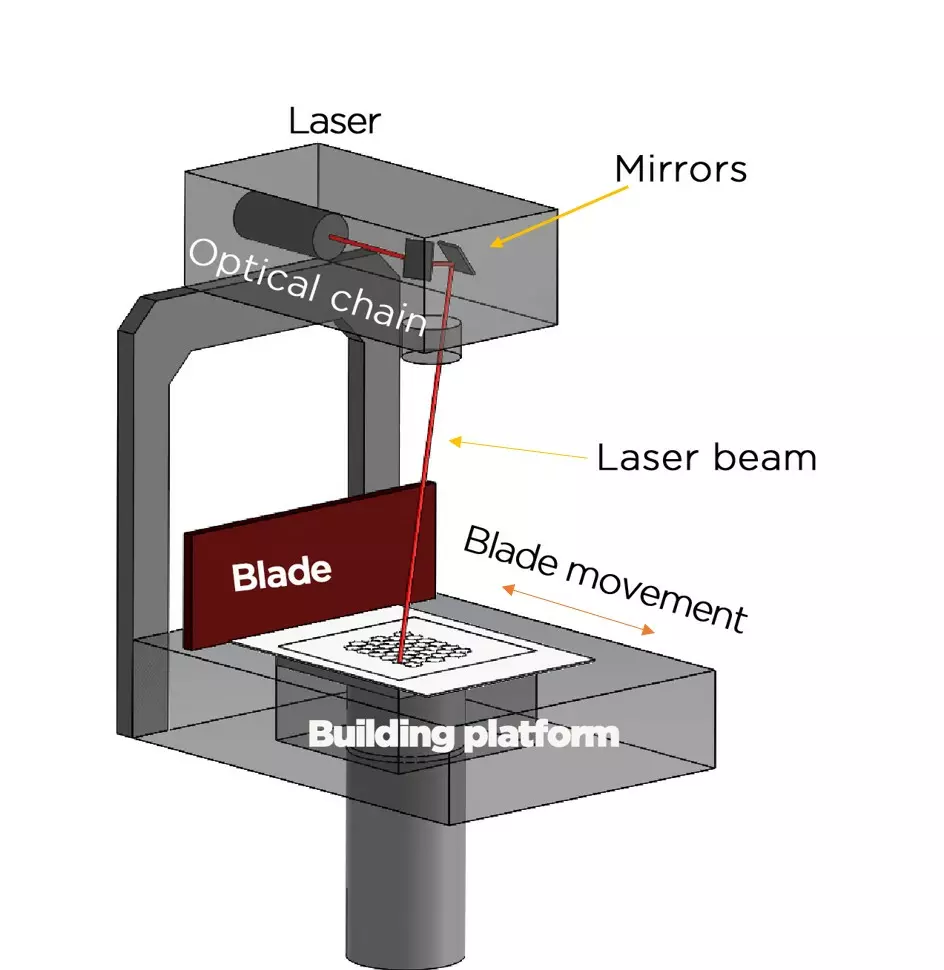
Descriptive scheme of 3DCERAM SLA Technology

After printing, operators remove uncured slurry and clean the green part either manually or with 3DCeram’s AUTO CERAKLEANER, an automated cleaning machine for 3D-printed ceramic parts. They then debind it to remove the organic binder. Sintering bonds the ceramic particles to form the finished part. The green body is fragile, and dimensions change during firing. Validate the firing cycle and dimensions with the chosen ceramic and part shape. The ceramic formulation and firing cycle set the final properties.

Start with the Finished Part

Choose Materials by Fired Properties

Define service conditions and acceptance requirements before shortlisting machines. Specify operating temperature, chemistry, vacuum or plasma exposure, electrical role, mechanical loads, wear and thermal cycling. Then set part size, smallest features, wall thickness, tolerance, surface finish, cleanliness and annual quantity. A wafer-handling fixture, a gas-flow component and a high-temperature insulator may all use technical ceramics, but they need different tests.

Select a formulation for the properties required in the final, sintered material. Alumina, zirconia, silicon nitride, aluminum nitride, silica-based materials and other ceramics offer different trade-offs. Request data for the exact formulation and firing cycle, then confirm that it can be printed on the target machine. Do not infer service temperature from a cured-slurry datasheet.

3DCeram also offers material solutions designed for open systems. CERA-BASE is a photopolymer binder system that enables users to develop their own ceramic suspensions using the ceramic powders of their choice. Cera XXX, on the other hand, is a range of ready-to-print ceramic slurries, available notably in alumina and zirconia and compatible with different photopolymerization wavelengths, providing greater flexibility across open platforms.

The geometry must fit the thermal route as well as the build platform. Thin walls and uniform sections can help control differential shrinkage; trapped slurry or closed cavities complicate cleaning and binder removal. Plan drainage paths, accessible surfaces and furnace supports early. Validate dimensional compensation on representative coupons or parts rather than relying on a universal shrinkage factor.

How to Evaluate an SLA Ceramic 3D Printer

A printer specification sheet helps shortlist equipment, but resolution alone cannot qualify a process. Compare each system against the real part, the planned workflow and the expected rate of accepted output.

Decision area What to confirm Why it matters Evidence to request
Part and volume Platform, orientation, spacing and parts per build. A nominal envelope does not show usable output or furnace capacity. Trial a representative batch and record accepted parts per cycle.
Features and accuracy Laser spot, layer range, minimum feature, repeatability and shrinkage data. Print resolution alone cannot predict final tolerances. Measure coupons and fired parts against the drawing.
Slurry and material Compatible ceramic grades, formulation data, supply and handling needs. Feedstock properties and machine settings are linked. Confirm the formulation and process window with the supplier.
Thermal workflow Cleaning, debinding, atmosphere, supports, inspection and finishing. This workflow sets yield and cost per accepted part. Run a pilot with batch records and dimensional checks.

Check the Entire Workflow

Ask suppliers to print representative geometry with the chosen material, then assess it after cleaning, debinding and sintering. Inspect fired dimensions, visible defects, repeatability across builds, finishing effort and batch yield. Include software and file preparation, material monitoring, operator training, maintenance, spare parts and process records in the review. If the site does not already have suitable cleaning and furnace capacity, include that equipment and its safety requirements in the installation plan.

Compare Ceramic SLA with Other Routes

Ceramic SLA is worth evaluating when a component needs fine detail, thin features, internal channels, customized geometry or consolidation of an assembly. It can remove mold lead time for prototypes and low-volume revisions, but the complete route still includes controlled firing and quality checks.

Compare SLA with DLP and LCD by exposure architecture, usable build area, slurry compatibility, feature limits and fired results. These light-based systems do not share one material window, and a projected pixel or screen pixel is not directly comparable with a laser spot. None of those resolution figures is a final-part tolerance. Ask vendors to demonstrate the same part and material.

Choose based on the features and production needs that matter, not a method label.

Calculate Total Cost of Ownership

Compare in-house printing with specialist outsourcing using cost per accepted part, not machine purchase price or raw feedstock price alone. Include printer and furnace capacity, material losses, cleaning labor, debinding and sintering cycles, fixtures, metrology, finishing, energy, maintenance, training, spares and expected yield. Estimate capacity using realistic build utilization and all downstream steps.

Outsourcing can help validate designs, establish firing windows and measure demand before investing. In-house production may make sense when recurring work, lead-time needs or process control justify the equipment and staff. There is no reliable universal break-even volume without part geometry, utilization, yield and local costs. Use a pilot to measure these inputs before making the business case.

3DCeram Systems and the Next Step

Within 3DCeram’s CERAMAKER range, the C101 EASY FAB provides a 100 x 100 x 150 mm build platform and is positioned for development and prototyping, with a scale-up route to larger printers. The C1000 FLEXMATIC has a 320 x 320 x 200 mm platform and is presented for larger parts and series production with semi-automated line integration. These are platform dimensions, not guaranteed part size or throughput; build layout and firing capacity must be checked against each design.

3DCeram formulates 3DMIX ceramic slurries for CERAMAKER printers and also describes on-demand formulations. For a machine shortlist, ask which material grades are available and what process data, training, cleaning and firing support accompany the selected configuration. Read the ceramic SLA process overview for a broader explanation of the technology.

Bring a representative CAD file, target material properties, operating environment, annual volume and critical tolerances to a technical discussion. Request a demonstration or sample-part evaluation, and agree in advance how the fired result will be measured. This gives engineering and procurement a shared basis for deciding whether to outsource a pilot or prepare an in-house workflow.

3DCERAM SLA portfolio

Advanced Ceramics for Semiconductors

How Alumina, Silicon Carbide and Aluminum Nitride support next-generation wafer processing

Advanced ceramics have become a core engineering requirement for semiconductor equipment manufacturers that need stable performance in extreme process conditions. As semiconductor process nodes move toward 2 nm and AI architectures drive higher thermal demands, ceramic components must withstand plasma exposure, harsh chemicals, high vacuum and rapid thermal cycling while maintaining tight dimensional control.

Why Advanced Ceramics Matter in Semiconductor Fabrication

Standard industrial materials can degrade, contaminate process chambers or lose dimensional stability under the combined stresses of modern wafer processing. Advanced technical ceramics provide the electrical insulation, chemical resistance, mechanical rigidity and thermal performance required by front-end fabrication equipment. These requirements also apply to ceramic end effectors, the robot blades used to transfer wafers between process chambers, cassettes and handling stations.

For process engineers and fab equipment OEMs, material selection is therefore more than a supply chain decision. It is a design constraint that affects chamber cleanliness, wafer uniformity, component lifetime and the ability to qualify equipment for increasingly demanding process windows.

Market Dynamics: The Quantitative Demand for Semiconductor Ceramics

The surge in capital expenditure (capex) for new fabrication facilities, particularly for AI chips and advanced nodes, is directly driving the consumption of semiconductor-grade ceramics. Every new fab adds demand for process chamber components, wafer handling parts, thermal management elements and replacement consumables.

According to Dataintelo, the global semiconductor ceramic fabricated parts market is valued at $9.4 billion in 2025 and is projected to nearly double, reaching $18.7 billion by 2034. This expansion represents a compound annual growth rate (CAGR) of 7.9% from 2026 to 2034.

Growth is heavily concentrated in wafer processing applications, which accounted for the highest revenue share, at 34.2%, in 2025. As foundries invest in extreme ultraviolet (EUV) lithography, advanced packaging and higher wafer throughput, demand for reliable liners, rings, plates and thermal management components scales with the installed equipment base.

The Core Trinity of Semiconductor Ceramics

The performance of vacuum components, electrostatic chucks (ESCs) and process chamber interiors relies primarily on three technical ceramics: Alumina, Silicon Carbide and Aluminum Nitride. Each material occupies a different position in the engineering trade-off between electrical behavior, thermal transport, chemical resistance, machinability and cost.

Material Selection

Material Key strengths Typical semiconductor applications Main engineering trade-off
Alumina (Al₂O₃) High-purity electrical insulation, rigidity, plasma resistance and mature supply chain. Chamber liners, end-effectors, lifting pins, focus rings, gas distribution plates and structural insulators. Reliable and cost-effective, but lower thermal conductivity than SiC or AlN.
Silicon Carbide (SiC) Very high hardness, thermal stability, thermal conductivity and resistance to thermal shock. Epitaxy and CVD components, susceptors and high-temperature process hardware. Grade selection and finishing are critical; machining is demanding and electrical behavior varies by grade.
Aluminum Nitride (AlN) High thermal conductivity combined with strong electrical insulation and a CTE close to silicon. Electrostatic chucks, wafer handling, heat sinks and high-power packaging. Excellent thermal performance, but cooling channels and tight geometries require precise engineering.

Alumina (Al2O3): The Industry Workhorse

Holding the largest material type share at 38.5% of the global semiconductor ceramic fabricated parts market in 2025, high-purity Alumina is the baseline standard for semiconductor tooling. It offers excellent dielectric strength, high mechanical rigidity and strong plasma resistance, which makes it suitable for insulating and structural parts exposed to demanding process chemistries.

Applications: In semiconductor manufacturing, alumina was used to produce customized lifting pins for CVD chambers, achieving full production qualification and enabling 600 validated sets to be delivered within weeks instead of months.

Read the full case study here

Silicon Carbide (SiC): Extreme Thermal Stability

Silicon Carbide represents the fastest-growing segment in this space, with a projected CAGR of 9.4% through 2034. Its exceptional hardness, extremely high thermal conductivity and near-perfect resistance to thermal shock make it valuable for high-temperature processes where dimensional stability and service life are critical.

Applications: Silicon Carbide is essential for high-temperature processes such as epitaxy growth and chemical vapor deposition (CVD), as well as other environments where the component must resist aggressive plasma and repeated thermal cycling.

Engineering Note: SiC’s low coefficient of thermal expansion helps limit thermally induced stress and maintain dimensional stability during rapid thermal processing, although the exact behavior depends on the SiC grade, wafer material and process temperature.

Aluminum Nitride (AlN): The Thermal Management Standard

As thermal budgets tighten, particularly for AI accelerator chips, Aluminum Nitride has become indispensable. Its ability to provide exceptionally high thermal conductivity, often exceeding 170 W/mK, while acting as a strong electrical insulator makes it a strong fit for heat-sensitive wafer handling and packaging systems.

Applications: Aluminum Nitride is the dominant material for electrostatic chucks (ESCs), high-power semiconductor packaging and specialized heat sinks. The key insight is the trade-off between electrical resistivity and thermal conductivity: AlN reaches a practical balance for modern wafer handling, while its internal cooling channels still require precise engineering and machining.

Why 3D Printing Is Now Necessary

Historically, ceramic components were manufactured through dry pressing, extrusion or slip casting, followed by green machining and high-temperature sintering. These methods remain effective for established geometries, but they become less flexible when next-generation semiconductor equipment requires internal channels, thin sections or integrated functions.

Machining technical ceramics is slow, expensive and restrictive when the component contains curved internal voids or complex surfaces. Stereolithography (SLA / VPP) ceramic 3D printing addresses this limitation by building the green part layer by layer from a digital model, followed by debinding and sintering.

Complex Internal Geometries and Conformal Cooling

The most significant limitation of traditional machining is the inability to create complex, curved internal voids. In advanced ESCs and showerheads, uniform gas distribution and fluid cooling are critical. Ceramic 3D printing enables the fabrication of conformal cooling channels, internal pathways that closely follow the contours of the component. This can support more uniform thermal dissipation across a 300mm wafer, helping to reduce edge defects and protect yield. The same design logic can benefit lightweight ceramic end effectors, where rigidity, low deflection, thermal stability and particle control are essential during robotic wafer transfer.

Functional Integration and Monolithic Design

Traditional assemblies often require joining multiple ceramic parts with brazing or mechanical fasteners, introducing potential leak points, dead zones and particle generation risks. Additive manufacturing allows 3DCeram Sinto to consolidate complex multi-part assemblies into single, monolithic structures. This level of functional integration can support cleaner operation in ultra-high vacuum (UHV) environments and extend component lifespan.

Engineering Note: Features such as diamond-inspired periodic open-cell structures, which maximize surface area for thermal or chemical reactions, cannot be machined in the same way as conventional forms. They must be grown layer by layer, making additive manufacturing a practical route to geometries that combine several functions in one ceramic component.

Agility in Tool Development and Rapid R&D

Fab equipment OEMs operate under demanding R&D timelines. Iterating a ceramic part conventionally can require expensive diamond-tooled molds and months of lead time. 3D printing eliminates the need for dedicated tooling, allowing engineers to move from a CAD file to a sintered, high-purity ceramic prototype in weeks and to iterate chamber liners, focus rings or custom wafer handling fixtures more quickly.

Partnering for Next-Generation Tooling

Meeting the demands of tomorrow's semiconductor fabs requires more than sourcing bulk material; it requires co-engineering geometries that push the boundaries of process performance. Material purity, print resolution, shrinkage compensation, debinding, sintering and finishing all contribute to the final component's behavior.

3DCeram Sinto provides stereolithography (SLA) ceramic 3D printing tailored explicitly for the semiconductor industry. By leveraging high-purity Alumina, Aluminum Nitride and Silicon Carbide, the engineering team helps OEMs pursue the thermal uniformity, plasma resistance and geometrical complexity required for sub-2nm nodes.

Conclusion: designing the next generation of semiconductor equipment

Advanced ceramics connect the electrical, thermal and chemical requirements of modern semiconductor fabrication. Alumina remains the dependable industry workhorse, Silicon Carbide serves the most thermally demanding environments and Aluminum Nitride provides a valuable balance of thermal conductivity and electrical insulation.

The adoption of ceramic 3D printing extends this material platform into more complex component designs. By enabling conformal cooling, monolithic integration and faster design iteration, additive manufacturing gives equipment engineers a practical route to improve performance while reducing tooling constraints.

Vat Photopolymerization for Advanced Ceramics

How ceramic SLA enables complex, high-performance parts from development to industrial production

Vat photopolymerization has become a key process for manufacturers that need advanced ceramic parts with complex geometries, fine details and high-quality surfaces. Often described as ceramic stereolithography or ceramic SLA, the technology combines the design freedom of additive manufacturing with the functional properties of technical ceramics after debinding and sintering. It is particularly relevant when conventional forming or machining would require costly tooling, extensive material removal or multiple assembled components

3DCeram Sinto SLA technology scheme

What Is Vat Photopolymerization in Ceramic 3D Printing?

Vat photopolymerization is an additive manufacturing process in which a light source selectively cures a photosensitive formulation. For ceramic applications, the formulation is a slurry containing a mix of fine ceramic powder and photopolymer resin. The printer creates a green part, which then undergoes cleaning, debinding and sintering to become a dense ceramic component for the most demanding applications. 3DCeram’s slurries contain 50–60% ceramic load content, supporting the shrinkage control.

The complete workflow starts with a CAD model. The geometry is oriented, supported when necessary and scaled to compensate for shrinkage. During printing, a laser cures each layer. The green part is then cleaned carefully before the organic is removed during debinding step. Finally, sintering consolidates the ceramic microstructure. Optional grinding, lapping or polishing may be used when a specific dimensional tolerance or surface condition is required. Typical layer thicknesses range from 25 to 100 µm.

Why the thermal steps matter?

Printing is only one stage of ceramic additive manufacturing. Debinding must remove the organic system without creating internal pressure that could cause cracks or deformation. Sintering then produces the final density and properties, but also generates dimensional shrinkage. The typical linear shrinkage is approximately 15-25%, depending on the material. For industrial users, reliable dimensional compensation therefore depends on calibrated material data, stable printing conditions and controlled furnace cycles.


Key Benefits for Advanced Ceramic Components

Fine features, smooth surfaces and design freedom

Ceramic vat photopolymerization is well suited to parts that combine fine features, thin walls, internal channels, lattices or intricate flow paths. The process can deliver smoother as-printed surfaces and finer geometric detail than powder-based or extrusion-based ceramic AM methods. This capability supports near-net-shape production and may reduce the amount of finishing required on complex surfaces. The smallest printable feature size in the XY plane can reach 50–150 µm, with as-sintered surface roughness typically around Ra 1–2 µm.

The technology also enables engineers to reconsider the part itself. Internal channels can be integrated into thermal or fluid-management components; porous or lattice regions can be added; and several functions may be consolidated into one printed geometry. These benefits are most valuable when complexity creates performance, reduces assembly or eliminates tooling rather than when the component is simple and already economical to press or mold.

A flexible route from R&D to production

Because the process starts from a digital file, designs can be revised without manufacturing a new mold. This makes ceramic SLA relevant for R&D, design qualification, prototypes, bridge production, short series and high-mix manufacturing. Productivity is influenced by build utilization, part height, furnace capacity, cleaning time and yield. Our comprehensive product range provides a smooth and scalable path from prototyping to industrial production.


How 3DCeram Applies Vat Photopolymerization

C101 EASY FAB: development with a direct scale-up path

The C101 EASY FAB illustrates how the same ceramic SLA approach can support both development and industrialization. Its 100 x 100 x 150 mm build platform is intended for developing and producing parts before scaling them to larger 3DCeram systems. The machine uses a one-piece granite structure combining mechanical and optical elements for long-term stability. Slurry delivery is controlled through a peristaltic pump and a pressurized material tank that supplies only the quantity required for the run. Real-time production monitoring and the availability of 3DCeram's CERIA system complete this development-to-production positioning. The machine can start a print with as little as 10 mL of ceramic slurry.

Full plate of cartillage scrapper produced on the C101 EASY FAB
Full batch of cartillage scraper produced on the C101 EASY FAB

C1000 FLEXMATIC: larger builds and semi-automated production

For larger parts or series production, the C1000 FLEXMATIC provides a 320 x 320 x 200 mm build platform and can be configured with two or three lasers according to the targeted productivity level. Its removable tank is designed to integrate printed-part processing into a semi-automated line. The machine also has an automated recycling of uncured material and a semi-automated cleaning step. Using top-down SLA, the system is designed to require few or no supports, simplifying post-print operations.  The 45 L pressurized material tank provides extended printing autonomy, enabling longer uninterrupted production runs.

Together, the C101 EASY FAB and C1000 FLEXMATIC show a practical scale-up logic: establish the material, geometry and process on a compact platform, then transfer the project to a larger industrial system while retaining a related material-feeding and process philosophy.

CERAMAKER Printers Range

3DCeram C101 EASY FAB ceramic 3D printer

C101 EASY FAB

3DCeram C1000 FLEXMATIC ceramic 3D printer

C1000 FLEXMATIC

Dimensions
(W × D × H)
1020 × 1005 × 1976 mm
1150 × 1850 × 1950 mm
Build Platform
100 × 100 × 150 mm
320 × 320 × 200 mm
Lasers
1
1 / 2 / 3
Parts produced on C101 EASY FAB
4 parts in 1h20 — 20 min / part
Parts produced on C1000 FLEXMATIC
48 parts in 6h10 — 7.7 min / part

Limitations and Engineering Considerations

Vat photopolymerization is not a push-button substitute for conventional ceramic processing. Green parts remain fragile during cleaning, support removal and transfer. Non-uniform wall thicknesses can produce differential shrinkage and warpage, while enclosed volumes may trap resin or gases. Designs should therefore avoid abrupt section changes, account for drainage and debinding, and use appropriate sintering supports when needed.

Material behavior is equally important. Density and mechanical properties can approach those of conventionally formed ceramics when the formulation and process are optimized, but pores, microcracks, surface damage or non-uniform thermal treatment can reduce performance. Safety-critical applications may require conservative design factors, extensive testing, traceability and formal qualification.


Industrial Applications of Ceramic Vat Photopolymerization

The strongest applications are those where advanced ceramic properties and geometric complexity are both essential. In semiconductor manufacturing, ceramic components can serve in wafer handling, etching, deposition and high-temperature environments. In aerospace and New Space, potential uses include scientific instruments, ceramic antennas and supports, optical components and thrusters. Green-hydrogen systems can benefit from corrugated or channel-rich geometries that increase exchange area and withstand demanding pressure conditions.

Biomedical applications include dental, orthopedic and reconstructive components, particularly when patient-specific geometry or controlled porosity is required. Other relevant areas include wear-resistant nozzles, seals, high-temperature fixtures, chemically resistant tooling and ceramic parts for thermal or electrical management. 3DCeram's material portfolio includes oxide and non-oxide formulations such as alumina, zirconia, silica-based material, hydroxyapatite, tricalcium phosphate, cordierite, aluminum nitride and silicon nitride. Suitability must be confirmed for each application and machine configuration.

Material selection is a critical part of ceramic additive manufacturing. Alumina and zirconia offer different combinations of strength, toughness and electrical performance, while technical ceramics such as silicon nitride, aluminum nitride and cordierite are selected for demanding thermal or dielectric environments. The table below summarizes indicative properties of materials available for ceramic vat photopolymerization; the final values depend on the formulation, printing parameters, debinding and sintering cycle.

Indicative properties of selected technical ceramics

Material
Density (g/cm³) CTE (ppm/K) Bending Strength (MPa) Fracture Toughness (MPa·m½) Thermal Cond. (W/m·K) Rel. Permittivity ε_r Dielectric Strength (kV/mm) High-Temp Res.
Alumina (Al₂O₃ 99.8%) 3.9 7–8 300–400 3–4 20–30 9–10 12–15 ~1600°C
Zirconia 3Y-TZP 6.0 10–11 900–1200 7–10 2–3 25–30 8–12 1000–1200°C
ATZ (Al₂O₃–ZrO₂) 4.1–4.3 8–9 500–900 4–6 15–25 12–15 10–12 1400–1500°C
Si₃N₄ 3.2 3–4 700–1000 6–10 20–30 7–8 10–13 1200–1400°C
AlN 3.3 4–6 250–350 2–3 140–180 8–9 12–15 ~800–1000°C
Cordierite 2.5–2.6 0–2 80–120 1–1.5 3–5 5–6 8–10 1100–1200°C

Note: values are indicative and may vary according to material grade, part geometry, orientation, printing parameters and thermal treatment. Please consult 3DCeram Sinto for application-specific material data.


When Should Manufacturers Choose Ceramic SLA?

Vat photopolymerization is a strong candidate when the part requires fine detail, internal channels, thin sections, high surface quality or customization, and when eliminating tooling creates clear value. It is less attractive for very simple, high-volume shapes that are already cost-effective to press or injection mold, or for parts that exceed the available build envelope. A realistic business case should include material, printing, cleaning, furnace cycles, inspection, finishing and expected yield.


Conclusion: turning complex ceramic designs into industrial parts

Ceramic vat photopolymerization connects digital design with the performance of sintered technical ceramics. Its value lies in producing geometries that are difficult to machine or form conventionally while supporting faster iteration and a tooling-free route to small and medium series. Success, however, depends on mastering the complete chain from slurry and printing parameters to debinding, sintering and quality assurance.

To evaluate how this approach could fit a specific component or production roadmap, discover 3DCeram Sinto's C101 EASY FAB and C1000 FLEXMATIC ceramic 3D printing solutions.

Join 3DCeram Sinto at Ceramitec Munich!

In just a few days, the 3DCeram Sinto team will head to Munich for the international trade fair for ceramics and, among others, technical ceramics: Ceramitec.

The opportunity for us to reveal our latest innovations. New materials, new proposals to facilitate and save on production costs on certain steps of the process.

Meet us from March 24 to 26, 2026, in Hall A6 – Stand 113/214 to discuss your projects and requirements. Our team will provide the insights you need to make the right choices and present our wide range of additive manufacturing options for technical ceramics.

Come and discover how 3DCeram Sinto supports you from prototyping to large-scale production in demanding markets such as aerospace, defense, medical, energy, and electronics.

At our booth, you will find:

One of the highlights of the show:

Richard Gaignon, CEO of the company, will be speaking at a round table dedicated to the industrialization of ceramic 3D printing. This panel, entitled "Scaling 3D Printed Technical Ceramics in Advanced Production," will bring together tech developers and industrial end-users to address real-world manufacturing challenges in what promises to be a rich and exciting debate.

Don’t miss the conferences featuring 3DCeram Sinto:

  1. Proposed and moderated by Ceramic Applications

"Production of small and medium series by additive manufacturing: automation and AI for better profitability"

Speaker: Eric Louradour (Business Developer)

Date: Tuesday, March 24, from 11:30 am to 11:50 am

Location: Hall A6 – A6.542

  1. Next-gen Ceramics: Powering the Future of Aeronautics Defence & Space – Proposed by the Pôle Européen de la Céramique

"Industrializing ceramics: how nitrides and automation redefine additive manufacturing"

Speaker: Maxence Bourjol (Sales Director)

Date: Tuesday, March 24, from 2:30 pm to 3:30 pm

Location: Hall A6 – A6.542

How to attend?

Free invitations are available upon request at info@3dceram.com (limited quantities available).

Looking forward to seeing you there!

Automated Post-Processing for Ceramic 3D Printing | Auto Cerakleaner

Here it is! The AUTO CERAKLEANER, our new automated cleaning machine dedicated to 3D printed ceramic parts. It is designed to optimize your production line and reduce your manufacturing costs per part.

Why choose the AUTO CERAKLEANER?

The AUTO CERAKLEANER is not just a cleaning machine; it is a performance driver for your workshop. It allows you to maximize your output while guaranteeing consistent quality.

Save time: Clean your parts faster than with manual cleaning (see table below).

Reduce your operator time: A very short intervention is needed to get parts ready for firing.

Safety & HSE: Protect your talent by minimizing prolonged exposure to solvents.

Preserve your parts: Its cleaning system with low mechanical stress limits the risk of scrap and breakage.

Efficiency proven by numbers The comparison between manual cleaning and the AUTO CERAKLEANER is undeniable:

A commitment to sustainability (CSR)

In addition to drastically reducing your operational costs (OPEX), the AUTO CERAKLEANER aligns with your sustainable development goals. Our AUTO CERAKLEAN solvent allows for multiple cleaning cycles before it needs to be renewed.

Ready to automate your success?

Download the product flyer here!

Contact us to discover how the AUTO CERAKLEANER can optimise your production line.

Email: info@3dceram.com

Scaling medical innovation with ceramic 3D Printing

In the rapidly evolving medical technology sector, the ability to move from R&D to industrial-scale production is a decisive competitive advantage. We spoke with G. Surgiwear Ltd., a leading company in the Indian medical and surgical field, about their journey with 3DCeram and the adoption of ceramic 3D printing.

Q: Could you tell us more about your company and your activities in the medical field?

A: We specialize in developing and manufacturing advanced solutions for the medical and surgical sector, including cranial implants, intervertebral cages, and a variety of bone substitutes. Our mission is to bring high-quality, biocompatible implants to market, combining innovation with patient safety.

Q: What led you to consider ceramic 3D printing?

A: For us, ceramic additive manufacturing is a strategic technology. It allows us to design complex geometries. We also see it as a bridge between research and full-scale production, which is a key part of our long-term vision.

Q: Why did you choose 3DCeram?

A: The choice was quite natural. We were impressed by 3DCeram’s 20 years of experience in the medical field and their clinical trials in collaboration with the CHU of Limoges. That heritage is rare and reassured us that we were investing not only in equipment, but in a partner with a biomedical expertise.

Another deciding factor was their top-down stereolithography technology, which ensures the level of detail and surface quality required for our market. Additionally, the software environment of their printers gives us the flexibility to optimize our process for future developments.

Q: How has your experience been with the technology so far?

A: We are currently in the R&D phase, using our 101 EASY FAB printer to produce prototypes and validate designs. The machine has been reliable, easy to use, and delivers excellent print quality. We also appreciate the technical support provided at the very beginning by SRT and 3DCeram, which has made the adoption smooth.

Q: What applications are you currently focusing on?

A: Our focus is primarily on custom medical implants, including cranial plates, spinal cages, and other orthopedic devices. We follow standard post-processing protocols — cleaning, debinding, sintering — and the quality control procedures to ensure the parts meet our medical-grade standards.

Q: What are your long-term objectives with ceramic 3D printing?

A: Our vision is to scale up from R&D to industrial production. We see 3DCeram’s technology as a key enabler for achieving that. With their expertise, the top-down technology, and proven results in the medical sector, we feel well-positioned to develop innovative solutions that will make a real difference for patients and surgeons on the Indian market.

Q: Any advice for other companies considering this technology?

A: Choose a partner who understands your industry. In our case, 3DCeram’s biomedical expertise and their ability to deliver both the tools and the know-how have been crucial. This is not just about printing parts — it’s about building a foundation for the future of medical manufacturing.

3DCeram Sinto at Formnext: Industrial Ceramic 3D Printing Serving Industry

From November 18 to 21 in Frankfurt (Hall 11.1 – Stand C68), 3DCeram Sinto reaffirms its mission: to provide manufacturers with a relevant and industrial-grade ceramic 3D printing offer, designed to meet the requirements of serial production.
With more than 20 years of expertise in ceramic additive manufacturing, 3DCeram Sinto delivers solutions tailored to real industrial needs, from R&D to full-scale production. The focus: precision, reliability, and cost efficiency.

Our range of printers has been designed to evolve with your requirements:

C1000 FLEXMATIC: a semi-automated printer designed for the serial production of ceramic parts – featuring a 320 × 320 × 200 mm build platform, a removable tank for recycling unused material, immediately reintegrated into the production cycle.

C3601 ULTIMATE: a large-format ceramic 3D printer — the largest build platform on the market, ideal for producing massive parts in a single piece, with high density and outstanding detail resolution.

3DCeram has developed a complete printer portfolio ensuring the most suitable solution for each use case, whether for small series, large-format components, or R&D phases with the C101 LAB.

3DCeram’s proprietary AI, CERIA, goes far beyond a simple assistant:

CERIA Set checks files, prepares the build platform, and generates optimized printing parameters.

On a system like the C3601 ULTIMATE, CERIA Set enables the printing of large parts in a single run, with a high success rate — increasing productivity while lowering costs.

With CERIA, 3DCeram Sinto places artificial intelligence at the core of industrializing ceramic 3D printing.

It streamlines workflows, reduces iterations, and secures processes — a key lever for manufacturers targeting reliable and scalable integration.

CERIA the AI for AM ceramics

We also provide a broad portfolio of technical ceramics — oxides (alumina, zirconia, etc.) and non-oxides (aluminum nitride, silicon nitride) — all engineered to ensure consistent, precise printing on our machines. This versatility allows us to meet the requirements of industries such as aerospace, energy, biomedical, and defense, where specific mechanical, thermal, or biocompatible properties are critical.

3DCeram offers a continuum of solutions:

All supported by training, maintenance, R&D services, and integrated software such as CPS 2.0, Build-It, and CERIA.

And also :

At Formnext, we will showcase proven, tangible solutions that transform ceramic 3D printing into a reliable, competitive, and scalable production tool.

Mastering Large-Scale Technical Ceramics – Key Insights from the 3DCeram x Bosch Webinar

In a groundbreaking webinar hosted by 3Dnatives, Maxence Bourjol, Head of Sales at 3DCeram, and Johannes Noll, Development Engineer at Bosch Advanced Ceramics, explored the revolutionary capabilities of laser-based ceramic additive manufacturing for producing large-scale, high-performance ceramics in series production.

This insightful session highlighted how this cutting-edge technology is transforming industries such as aerospace, semiconductor, and beyond, and its potential to redefine high-precision ceramic manufacturing.

Pushing the Boundaries of Large-Scale Ceramic Production

Laser-based additive manufacturing is fundamentally changing the way high-precision ceramic parts are produced. This technology allows manufacturers to achieve unparalleled flexibility in design and scalability while maintaining the unique material properties of ceramics, such as high temperature resistance, hardness, and corrosion resistance.

Maxence Bourjol and Johannes Noll shared real-world applications demonstrating how laser-based printing is enabling industries to meet the growing demand for complex, high-performance ceramic components essential in high-stress environments.

Key Technological Requirements for Success

The webinar focused on the critical technological requirements for success in laser-based ceramic additive manufacturing. Experts from 3DCeram and Bosch emphasized the importance of precise control over laser parameters, material formulations, and post-processing techniques to achieve high-quality ceramics that meet rigorous industry standards.

For industries like aerospace, where components must withstand extreme conditions, this technology opens the door to producing lightweight yet durable ceramic parts that would otherwise be challenging to create using traditional methods.

Laser-Based Technology in Aerospace and Semiconductor Applications

A key highlight of the webinar was the application of laser-based ceramic printing in aerospace and semiconductor industries. In aerospace, the ability to produce lightweight and thermally resistant ceramic components using 3D printing is transforming the design and production of critical parts such as turbine blades and nozzles.

Similarly, in the semiconductor industry, laser-based ceramics offer enhanced precision and reliability, key factors for the performance of next-generation technology.

How 3DCeram is Driving Innovation in Laser-Based Ceramic Printing

At the forefront of these innovations is 3DCeram’s advanced SLA (Stereolithography) technology, which allows for precise layer-by-layer fabrication of complex ceramic structures.

By integrating laser printing capabilities with optimized material formulations and advanced process control, 3DCeram is helping industries push the limits of ceramic component production.

Don’t Miss Out – Watch the Full Webinar for In-Depth Insights!

If you missed the live session or want to revisit the valuable insights shared, the full webinar is now available for on-demand viewing. It’s your chance to dive deep into the future of laser-based ceramic 3D printing and how it’s set to revolutionize industries that rely on high-performance ceramics.

🚀 Whether you’re in aerospace, semiconductor, or another industry that relies on cutting-edge materials, this webinar is a must-watch. Get inspired and discover how you can be part of the next wave of industrial innovation!

🔗 Click here to watch the full webinar

Opening the Biomedical 3D Printing, a webinar gives key insights from the YCN

3D Printing is pushing the boundaries of the biomedical field, and the latest Young Ceramists Network (YCN) webinar provided an in-depth look at the cutting-edge advancements in 3D-printed implants. Charlie Clark, an expert from 3DCeram, shared valuable insights into the transformative potential of ceramic additive manufacturing for medical applications. 

🔗 Watch the full webinar here: YCN #19 - 3D Printing in Biomedical applications 

Pioneering 3D-Printed skull implants 

Since 2005, 3DCeram has been at the forefront of 3D-printed medical implants, with more than 15 custom skull implants successfully completed for patients at the CHU de Limoges. This webinar explored the advantages of 3D printing in cranial reconstruction, highlighting the ability to create implants with varying densities to optimize mechanical strength, osteointegration, and surgical fixation. Real-world cases demonstrated how these customized implants seamlessly integrate with bone structure, improving patient outcomes. 

Advancements in Zirconia-Based ceramics 

The session also covered groundbreaking research conducted in collaboration with INSA Lyon on cerium-stabilized zirconia. This innovative ceramic material significantly improves the longevity of biomedical implants by addressing aging-related degradation, which has been a major challenge in traditional zirconia implants. The research aims to enhance the mechanical properties and durability of implants, potentially eliminating the need for revision surgeries. 

Click down below to watch an interview about our collaboration with the surgeon we worked with to use the first skull implants on real life cases :

A new era for spinal cages 

Another key highlight was the collaboration between 3DCeram and a customer in Australia to develop next-generation spinal cages using a novel strontium-based ceramic material. Traditionally, spinal cages require bone grafting, leading to additional surgical procedures. This new material not only enhances bioactivity and bone fusion but also has the potential to eliminate the need for autografts, simplifying spinal surgery and improving patient recovery. 

The power of SLA technology in medical innovation 

Charlie Clark also detailed the unique benefits of SLA (Stereolithography) technology used by 3DCeram. This top-down approach enables precise layer-by-layer fabrication, allowing the production of intricate lattice structures that enhance biocompatibility and mechanical performance. The combination of advanced formulations, optimized printing parameters, and post-processing techniques ensures that ceramic implants meet the highest industry standards, with examples that speak for themselves. 

Watch the webinar for more insights 

For those interested in learning more about these groundbreaking innovations in biomedical 3D printing, the full webinar is available on our YouTube channel. Discover how ceramic additive manufacturing is pushing the boundaries of medical technology and shaping the future of personalized healthcare.